
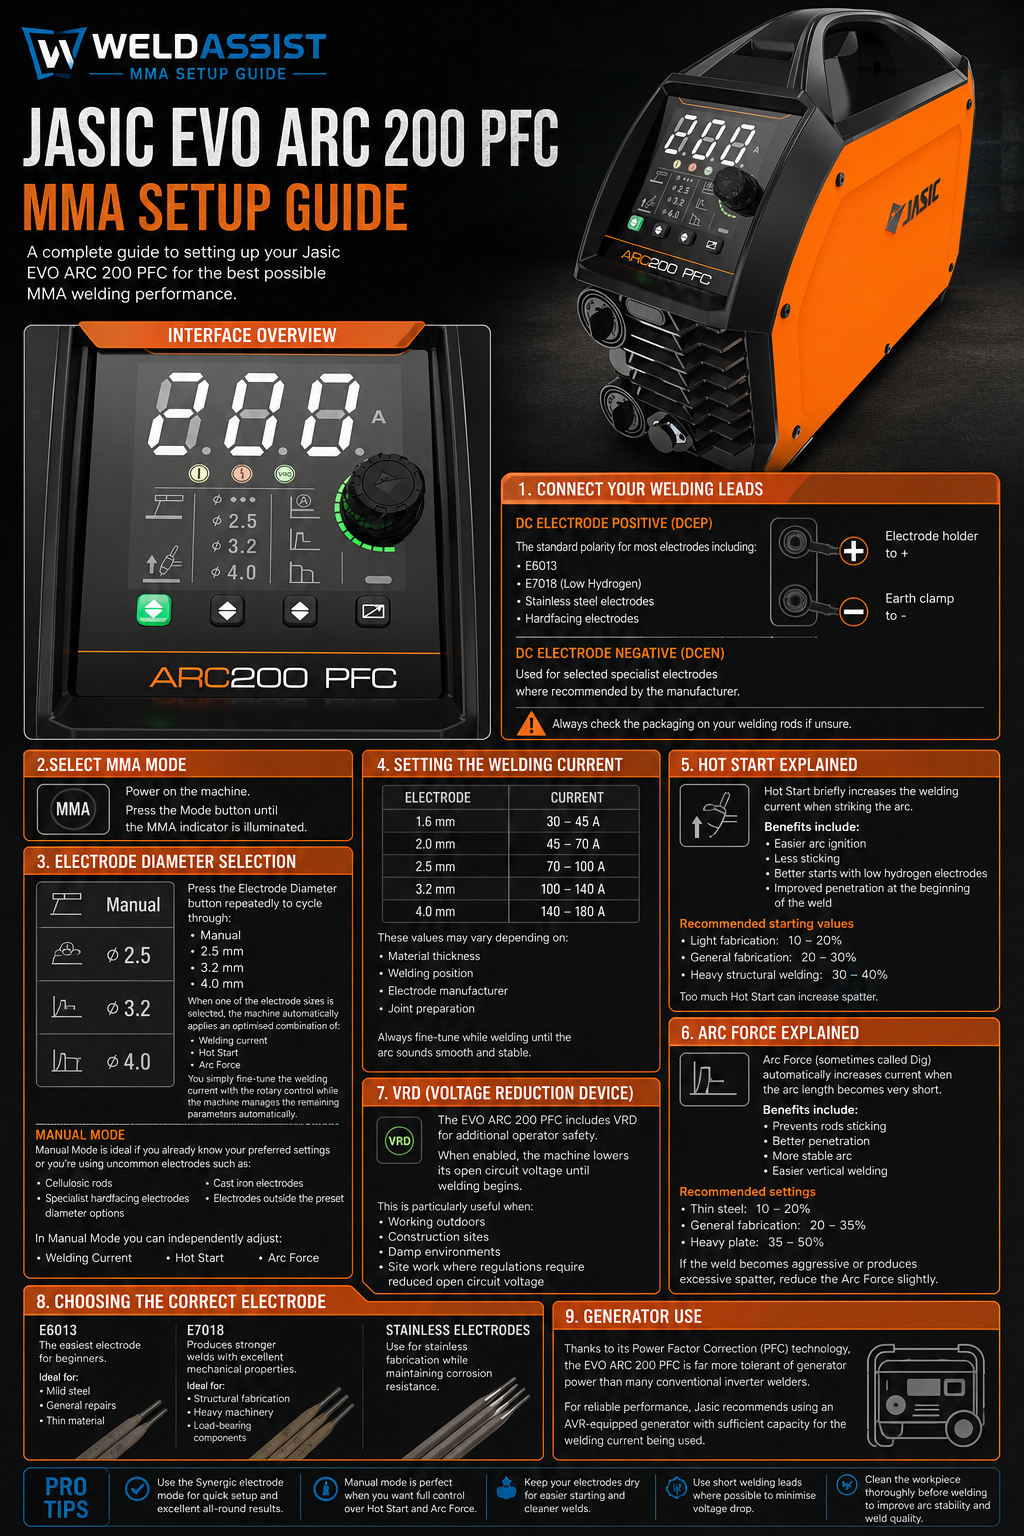
The Jasic EVO ARC 200 PFC is one of the most advanced portable MMA welders on the market. With PFC (Power Factor Correction), synergic electrode selection and excellent arc characteristics, it is equally at home in the workshop or on site.
If you’ve just unboxed your machine or want to understand what every button does, this guide will walk you through the setup process and explain how to get the best performance from your welder.
Step 1 – Connect Your Welding Leads
The first step is choosing the correct polarity.
DC Electrode Positive (DCEP)
This is the standard polarity for most electrodes including:
- E6013
- E7018 (Low Hydrogen)
- Stainless steel electrodes
- Hardfacing electrodes
Connect:
- Electrode holder to +
- Earth clamp to –
DC Electrode Negative (DCEN)
Used for selected specialist electrodes where recommended by the manufacturer.
Always check the packaging on your welding rods if unsure.
Step 2 – Select MMA Mode
Power on the machine.
Press the Mode button until the MMA indicator is illuminated.
The display now changes to the MMA welding interface.
Step 3 – Understanding the Electrode Diameter Selection
One of the standout features of the EVO ARC 200 PFC is its Synergic Electrode Diameter Mode.
Instead of setting every parameter manually, you simply tell the machine which size electrode you’re using.
Press the Electrode Diameter button repeatedly to cycle through:
• Manual
• 2.5 mm
• 3.2 mm
• 4.0 mm
When one of the electrode sizes is selected, the machine automatically applies an optimised combination of:
- Welding current
- Hot Start
- Arc Force
You simply fine-tune the welding current with the rotary control while the machine manages the remaining parameters automatically. (JASIC)
When should you use Manual Mode?
Manual Mode is ideal if you already know your preferred settings or you’re using uncommon electrodes such as:
- Cellulosic rods
- Specialist hardfacing electrodes
- Cast iron electrodes
- Electrodes outside the preset diameter options
In Manual Mode you can independently adjust:
- Welding Current
- Hot Start
- Arc Force
giving experienced welders complete control over the arc. (JASIC)
Step 4 – Setting the Welding Current
A great starting point is:
Electrode – Current
1.6 mm – 30–45 A
2.0 mm – 45–70 A
2.5 mm – 70–100 A
3.2 mm – 100–140 A
4.0 mm – 140–180 A
These values may vary depending on:
- Material thickness
- Welding position
- Electrode manufacturer
- Joint preparation
Always fine-tune while welding until the arc sounds smooth and stable.
Step 5 – Hot Start Explained
Hot Start briefly increases the welding current when striking the arc.
Benefits include:
- Easier arc ignition
- Less sticking
- Better starts with low hydrogen electrodes
- Improved penetration at the beginning of the weld
Recommended starting values
Light fabrication:
10–20%
General fabrication:
20–30%
Heavy structural welding:
30–40%
Too much Hot Start can increase spatter.
Step 6 – Arc Force Explained
Arc Force (sometimes called Dig) automatically increases current when the arc length becomes very short.
Benefits include:
- Prevents rods sticking
- Better penetration
- More stable arc
- Easier vertical welding
Recommended settings:
Thin steel:
10–20%
General fabrication:
20–35%
Heavy plate:
35–50%
If the weld becomes aggressive or produces excessive spatter, reduce the Arc Force slightly.
Step 7 – VRD (Voltage Reduction Device)
The EVO ARC 200 PFC includes VRD for additional operator safety.
When enabled, the machine lowers its open circuit voltage until welding begins.
This is particularly useful when:
- Working outdoors
- Construction sites
- Damp environments
- Site work where regulations require reduced open circuit voltage
Step 8 – Choosing the Correct Electrode
E6013
The easiest electrode for beginners.
Ideal for:
- Mild steel
- General repairs
- Thin material
E7018
Produces stronger welds with excellent mechanical properties.
Ideal for:
- Structural fabrication
- Heavy machinery
- Load-bearing components
Store these rods dry as they readily absorb moisture.
Stainless Electrodes
Use for stainless fabrication while maintaining corrosion resistance.
Step 9 – Generator Use
Thanks to its Power Factor Correction (PFC) technology, the EVO ARC 200 PFC is far more tolerant of generator power than many conventional inverter welders.
For reliable performance, Jasic recommends using an AVR-equipped generator with sufficient capacity for the welding current being used. (
Pro Tips
✔ Use the Synergic electrode mode for quick setup and excellent all-round results.
✔ Manual mode is perfect when you want full control over Hot Start and Arc Force.
✔ Keep your electrodes dry for easier starting and cleaner welds.
✔ Use short welding leads where possible to minimise voltage drop.
✔ Clean the workpiece thoroughly before welding to improve arc stability and weld quality.
Final Thoughts
The Jasic EVO ARC 200 PFC combines portability with advanced digital control, making it an excellent choice for both beginners and experienced welders. Its synergic electrode diameter feature takes much of the guesswork out of setup, while Manual mode allows complete control when required.
Whether you’re carrying out workshop fabrication, site maintenance or structural steelwork, spending a few minutes setting the machine correctly will reward you with easier arc starts, reduced spatter and consistently higher-quality welds.
Leave a Reply